The MEI temperature and humidity monitoring system is an IoT solution that uses sensors SHT30 and controller STM32 to monitor environmental conditions in real time. Devices that support connection Wi-Fi or Ethernet (LAN), display temperature and humidity above 7-segment LED and Web/App platform. The system allows configuration of alarm thresholds, local horn activation and sending Push Notification when parameters exceed limits or the device has a problem. Data is stored offline when connection is lost and automatically syncs when the network is restored. In addition, the system supports user authorization, trend charts, history saving and report export Excel, PDF, CSV, effectively meeting the needs of environmental monitoring and management.
Factory temperature and humidity monitoring
Products
Factory temperature and humidity monitoring
MEI temperature and humidity monitoring system is an IoT solution developed to track, monitor and store real-time environmental data for factories, warehouses, clean rooms, laboratories, cold storage and areas requiring control of temperature and humidity conditions. The device uses digital sensors SHT30 has high precision and stability, combined with platform controller STM32, connection support Wi-Fi or Ethernet (LAN) to transmit data to the Web/App platform.
The system continuously collects temperature and humidity data, displayed directly on 7-segment LED display and Dashboard in real time, and provides trend charts, historical data and statistics to help users monitor, analyze and evaluate environmental conditions in each area. Administrators can configure warning thresholds for each parameter, delay time and warning mode according to user needs.
When the temperature or humidity exceeds the set threshold, the connection is lost or the device has a problem, the system will automatically activate. Warning horn in place and send instant notifications via Web/App Notification (Push Notification), helping operators quickly detect and handle problems. In addition, the system integrates functions Offline Data Logging, ensures data is not lost when Internet connection is lost and automatically synchronizes to the server as soon as the connection is restored.
Supported software platform user authorization, manage multiple devices on the same system, store operating history, alarm logs and export reports in various formats Excel, PDF, CSV by day, month or optional time period. With flexible scalability, high reliability and centralized management, the MEI solution effectively meets the environmental monitoring needs of modern industrial and manufacturing systems.
TECHNICAL SPECIFICATIONS
MEI temperature and humidity monitoring system is a specialized IoT solution developed to continuously monitor environmental conditions in factories, warehouses, clean rooms, laboratories, cold storage, data centers and areas that require high-precision temperature and humidity control. The device uses digital sensors SHT30 High stability, allowing simultaneous measurement of temperature and humidity with low errors, ensuring reliable data for management and monitoring.
The controller is developed on a microcontroller platform STM32, supports network connection Wi-Fi or Ethernet (LAN) to transmit real-time data to the Cloud platform via protocol MQTT. The system allows configuring the sampling cycle, data transmission cycle, update time and automatically synchronizes time with the server to ensure the accuracy of stored data.
The device continuously collects temperature and humidity data from the SHT30 sensor, directly displaying the measured value on the 7-segment LED display With high brightness, easy to observe at the scene. At the same time, data is transmitted to the Web/App platform for real-time display in the form of Dashboard, trend chart, data table and operating history, helping managers easily monitor environmental developments in each area.
The system allows flexible configuration of warning thresholds High, Low, High-High and Low-Low for each temperature and humidity parameter, and also supports Delay Time settings to eliminate false alarms due to instantaneous fluctuations. When the value exceeds the threshold or a device connection is lost, the system will activate horn and warning lights in place, and send instant notifications via Web/App Notification (Push Notification), Email or extended alert channels according to system configuration.
To ensure data is not lost in case of loss of Internet connection or Cloud server, the device integrates Offline Data Logging. All measured data will be saved in real time in memory and automatically Auto Synchronization to the server as soon as connectivity is restored, ensuring database integrity and continuity.
Supported software platform Multi-user management and access authorization by each level such as Administrator, Manager and Operator. Each user group is granted permission to view data, configure devices, change alarm thresholds, confirm alarms or export reports according to the authorized scope, helping to enhance security and control of the system.
All historical data is stored on the server, supporting search over time, displaying trend analysis charts and Export reports in Excel, PDF or CSV format by day, week, month or optional time period. Reports include temperature data, humidity, alarm history, equipment status, connection loss times, and operating logs, meeting quality management, data retrieval, and record keeping requirements in factories and manufacturing facilities.
With open architecture, flexible scalability and safe data storage mechanism, the MEI temperature and humidity monitoring system provides an accurate, stable and reliable environmental monitoring solution, contributing to improving management efficiency, minimizing risks in production and meeting requirements for controlling environmental conditions according to current standards.
Products for the same solution
Water and wastewater quality monitoring device (internal monitoring)
MEISync - CTG.100
BPS CONTROLLER – CT.400
Door monitoring
CNC machine monitoring
BPS Controller - CTG.300
LoraSync - LR.100
Remote sensor monitoring
Lora Node (Model: CT003)
AQUAMONITOR - DTG.800
SENSOR - DTG.100
SMART PRV - PRV.03
Fine particulate matter monitoring
Fire alarm monitoring
10-channel Wi-Fi/LoRa controller
PumpPerf - DTG.500
IoT Gateway (model: MEI_MT03)
BMS - CTG.050
MEISync - CTG.200
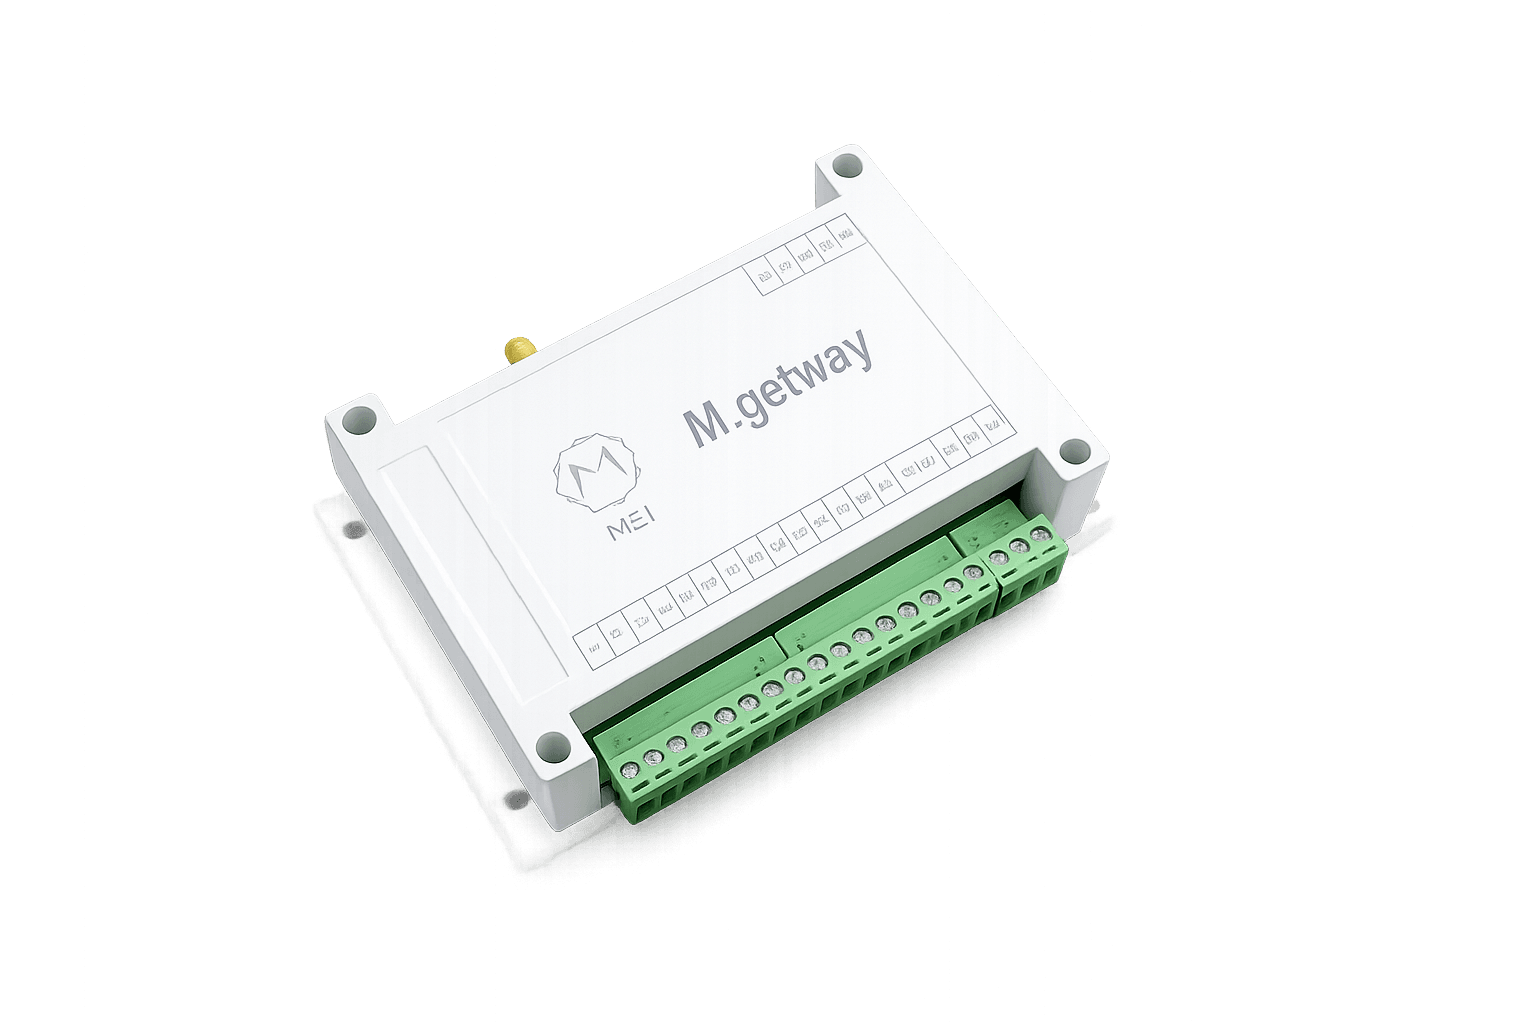
Industrial IoT Gateway
Support

- FAQ
- Resources
- Distributor
- Technical Support
MEIGROUP DOWNLOAD